What are the difficulties in controlling the thickness tolerance of polyimide film surface coated wi
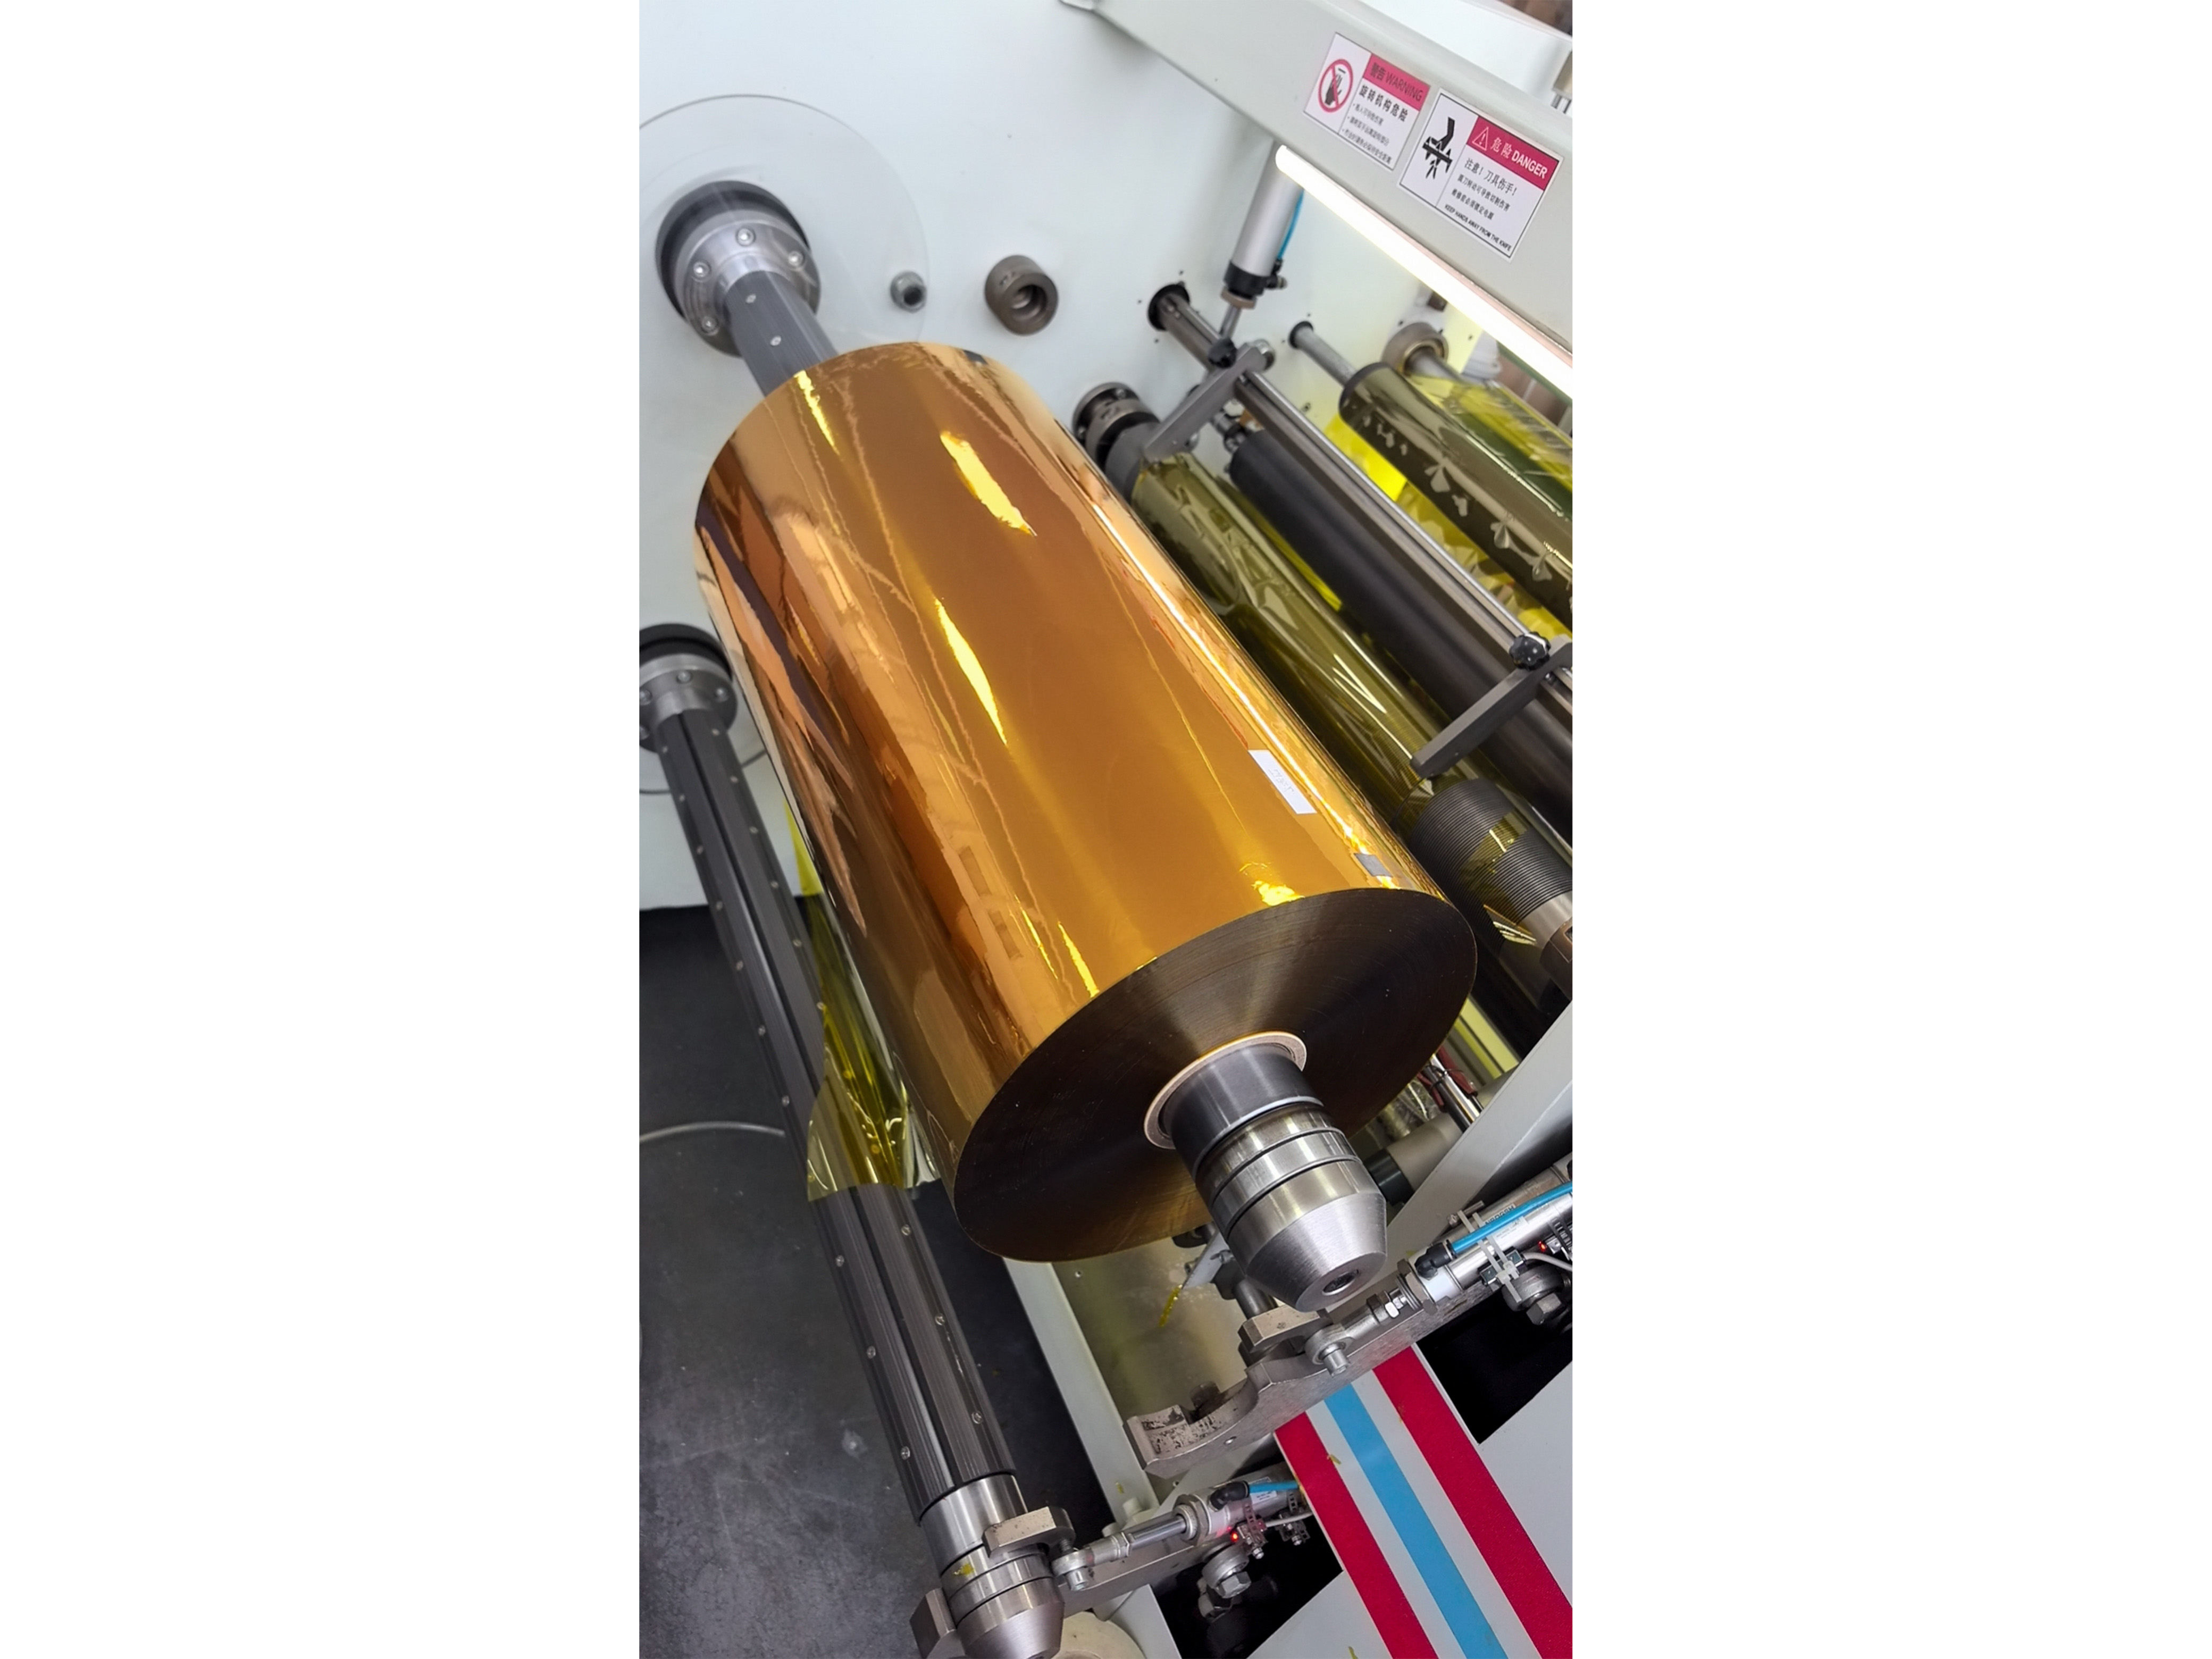
The surface of polyimide film is coated with graphite slurry and thermal conductive adhesive. The overall goal of tolerance control is to stabilize the coating thickness, ensure thermal conductivity uniformity, and avoid insulation/thermal performance fluctuations. The difficulties come from the combination of PI substrate characteristics, slurry system, coating process, and post curing, as follow
The surface of polyimide film is coated with graphite slurry and thermal conductive adhesive. The overall goal of tolerance control is to stabilize the coating thickness, ensure thermal conductivity uniformity, and avoid insulation/thermal performance fluctuations. The difficulties come from the combination of PI substrate characteristics, slurry system, coating process, and post curing, as follows:
1. Dimensional stability and tension sensitivity issues of PI substrate itself
PI film is resistant to high temperatures, but its rigidity is relatively weak, making it a thin soft film that is extremely sensitive to tension. During the film coating process, there is a slight fluctuation in tension, causing the film to be stretched and the coating area to deform horizontally and vertically; Even if the thickness meets the standard during coating, heating during the curing stage will cause thermal shrinkage of PI, resulting in synchronous deviation of coating thickness. At the same time, the PI film itself has small thickness tolerances, loose edges, and warping, and the thickness difference of the substrate itself will be directly superimposed on the coating, which is difficult to completely offset solely by the coating head. The rigidity of PET substrate is better, while the issue of PI will be more prominent. In addition, the surface energy of PI is relatively low, and even after corona discharge, uneven wetting of the slurry is prone to occur, and local leveling differences are converted into thickness deviations.
2. The rheological properties of graphite thermal conductive slurry are complex
Graphite thermal conductive adhesive/graphite slurry belongs to a system with high solid content and a high proportion of fillers (flake graphite, artificial graphite), high solid content, high viscosity, and strong thixotropy.
Static placement is prone to settling, graphite particles sink, and the solid content of the upper and lower slurries is inconsistent. Under the same coating gap, the discharge thickness is inconsistent before and after;
Shear thinning: During coating, the viscosity decreases under the shear action of the scraper and die head. After leaving the coating area, the viscosity quickly increases, and the leveling window is very short; Insufficient leveling results in uneven thickness, while excessive leveling can lead to a "thick edge effect" where the edges are thick and the middle is thin;
Graphite flakes have a large diameter, and large flake graphite is prone to getting stuck in mold heads and scraper gaps, causing local material shortages, stripes, and sudden thickness changes; Small particle graphite slurry has better flowability, but lower thermal conductivity efficiency.
The viscosity is significantly affected by temperature and stirring time, with slight fluctuations in workshop temperature and changes in slurry viscosity, directly leading to coating thickness drift.
3. Inherent limitations of coating methods
Mold head coating and scraper coating are the mainstream processes for PI thermal conductive film:
Scraper coating: It is greatly affected by the flatness, pressure, gap between the scraper and the film surface, and vibration of the scraper. The shaking of the soft substrate during film coating can easily cause striped thickness differences;
The narrow slot die coating requires high stability of the feeding pressure, and the pulse of the feeding pump and the bubbles in the pipeline can cause the discharge to fluctuate;
Graphite slurry with high filler properties is more prone to generating bubbles, which can break through the pores inside the coating and form local thickness anomalies. It is difficult to achieve complete uniformity in the horizontal distribution of the wide PI film slurry, and it is prone to thinning in the middle and thickening on both sides.
4. The difference in volume shrinkage during the curing process leads to a secondary deviation in thickness
Graphite thermal conductive adhesive contains solvents or resin matrix. During the drying, imidization/thermal curing stages, solvent evaporation and resin cross-linking curing will cause significant shrinkage of the coating.
The solvent content and packing density of different positions of the slurry are different, and the shrinkage rate is not consistent: in areas where the slurry is thick, there is more solvent and greater shrinkage, and the thickness of the finished product does not correspond linearly with the thickness of the newly coated wet film.
At the same time, the thermal expansion coefficients of PI film and graphite coating do not match. During the curing heating and cooling stages, interface stress will cause slight wrinkling and undulating of the coating, further amplifying the thickness tolerance; When severe, the coating may have ripples, and the thickness detection may fluctuate greatly.
5. Online detection and feedback lag, making closed-loop control difficult
Graphite coating itself is opaque, and ordinary optical thickness measurement is difficult to penetrate the coating. Beta rays and laser displacement thickness measurement are often used.
Laser thickness measurement is susceptible to interference from matte and rough textures on graphite surfaces, resulting in high reading noise;
Beta ray thickness measurement is stable, but the equipment cost is high and the response is slow, making it difficult to achieve real-time fine-tuning of the die gap;
In addition, with the high-speed feeding of soft film, there is a distance between the detection point and the coating head. When exceeding the tolerance is detected, a defective product has already been produced, and the lag is obvious.
6. The joint effects of interfaces, additives, and surface defects
PI corona attenuation, surface dust, and oil stains can cause local shrinkage and edge shrinkage of the slurry, resulting in point like thickness anomalies; Imbalanced addition of dispersants and wetting agents can exacerbate the instability of slurry flow. In addition, if the coating needs to be coated on both sides, after one side is coated and cured, the PI film has already undergone stress warping. When the second side is coated, the flatness of the substrate deteriorates, and the difficulty of tolerance control doubles.
 WeChat number:

 Home
 Product
 Wechat
 Telephone