What are the key process points to pay attention to when processing and cutting unidirectional polyi
Unidirectional polyimide film undergoes uniaxial stretching, with molecular chains oriented along the stretching direction. There are differences in mechanical and thermal properties between the two perpendicular directions, and the slitting process needs to be controlled based on the anisotropic characteristics of the material. The main process points are as follows:
Unidirectional polyimide film undergoes uniaxial stretching, with molecular chains oriented along the stretching direction. There are differences in mechanical and thermal properties between the two perpendicular directions, and the slitting process needs to be controlled based on the anisotropic characteristics of the material. The main process points are as follows:
1. Confirm the stretching direction of the film and plan the cutting layout
Before slitting, identify the longitudinal (stretching direction) and transverse (perpendicular stretching direction) directions of the film. Unidirectional PI film has higher tensile strength along the stretching direction, but relatively weaker transverse tear resistance. When typesetting, the cutting direction should be determined based on the customer's future usage direction to avoid direct force cutting along the horizontal direction and reduce the probability of irregular tearing and burrs on the film.
2. Control the unwinding tension to avoid stretching deformation
Unidirectional polyimide film is sensitive to tension. The tension during the unwinding and pulling stages should not be too high to prevent the film from being further stretched along the stretching direction, which may cause dimensional deviations in the finished product and thermal shrinkage deformation during subsequent use; At the same time, the tension should not be too low to prevent the film from deviating and wrinkling. Maintain stable tension throughout the entire process to reduce material stretching fluctuations caused by sudden tension changes.
3. Tool selection and edge status management
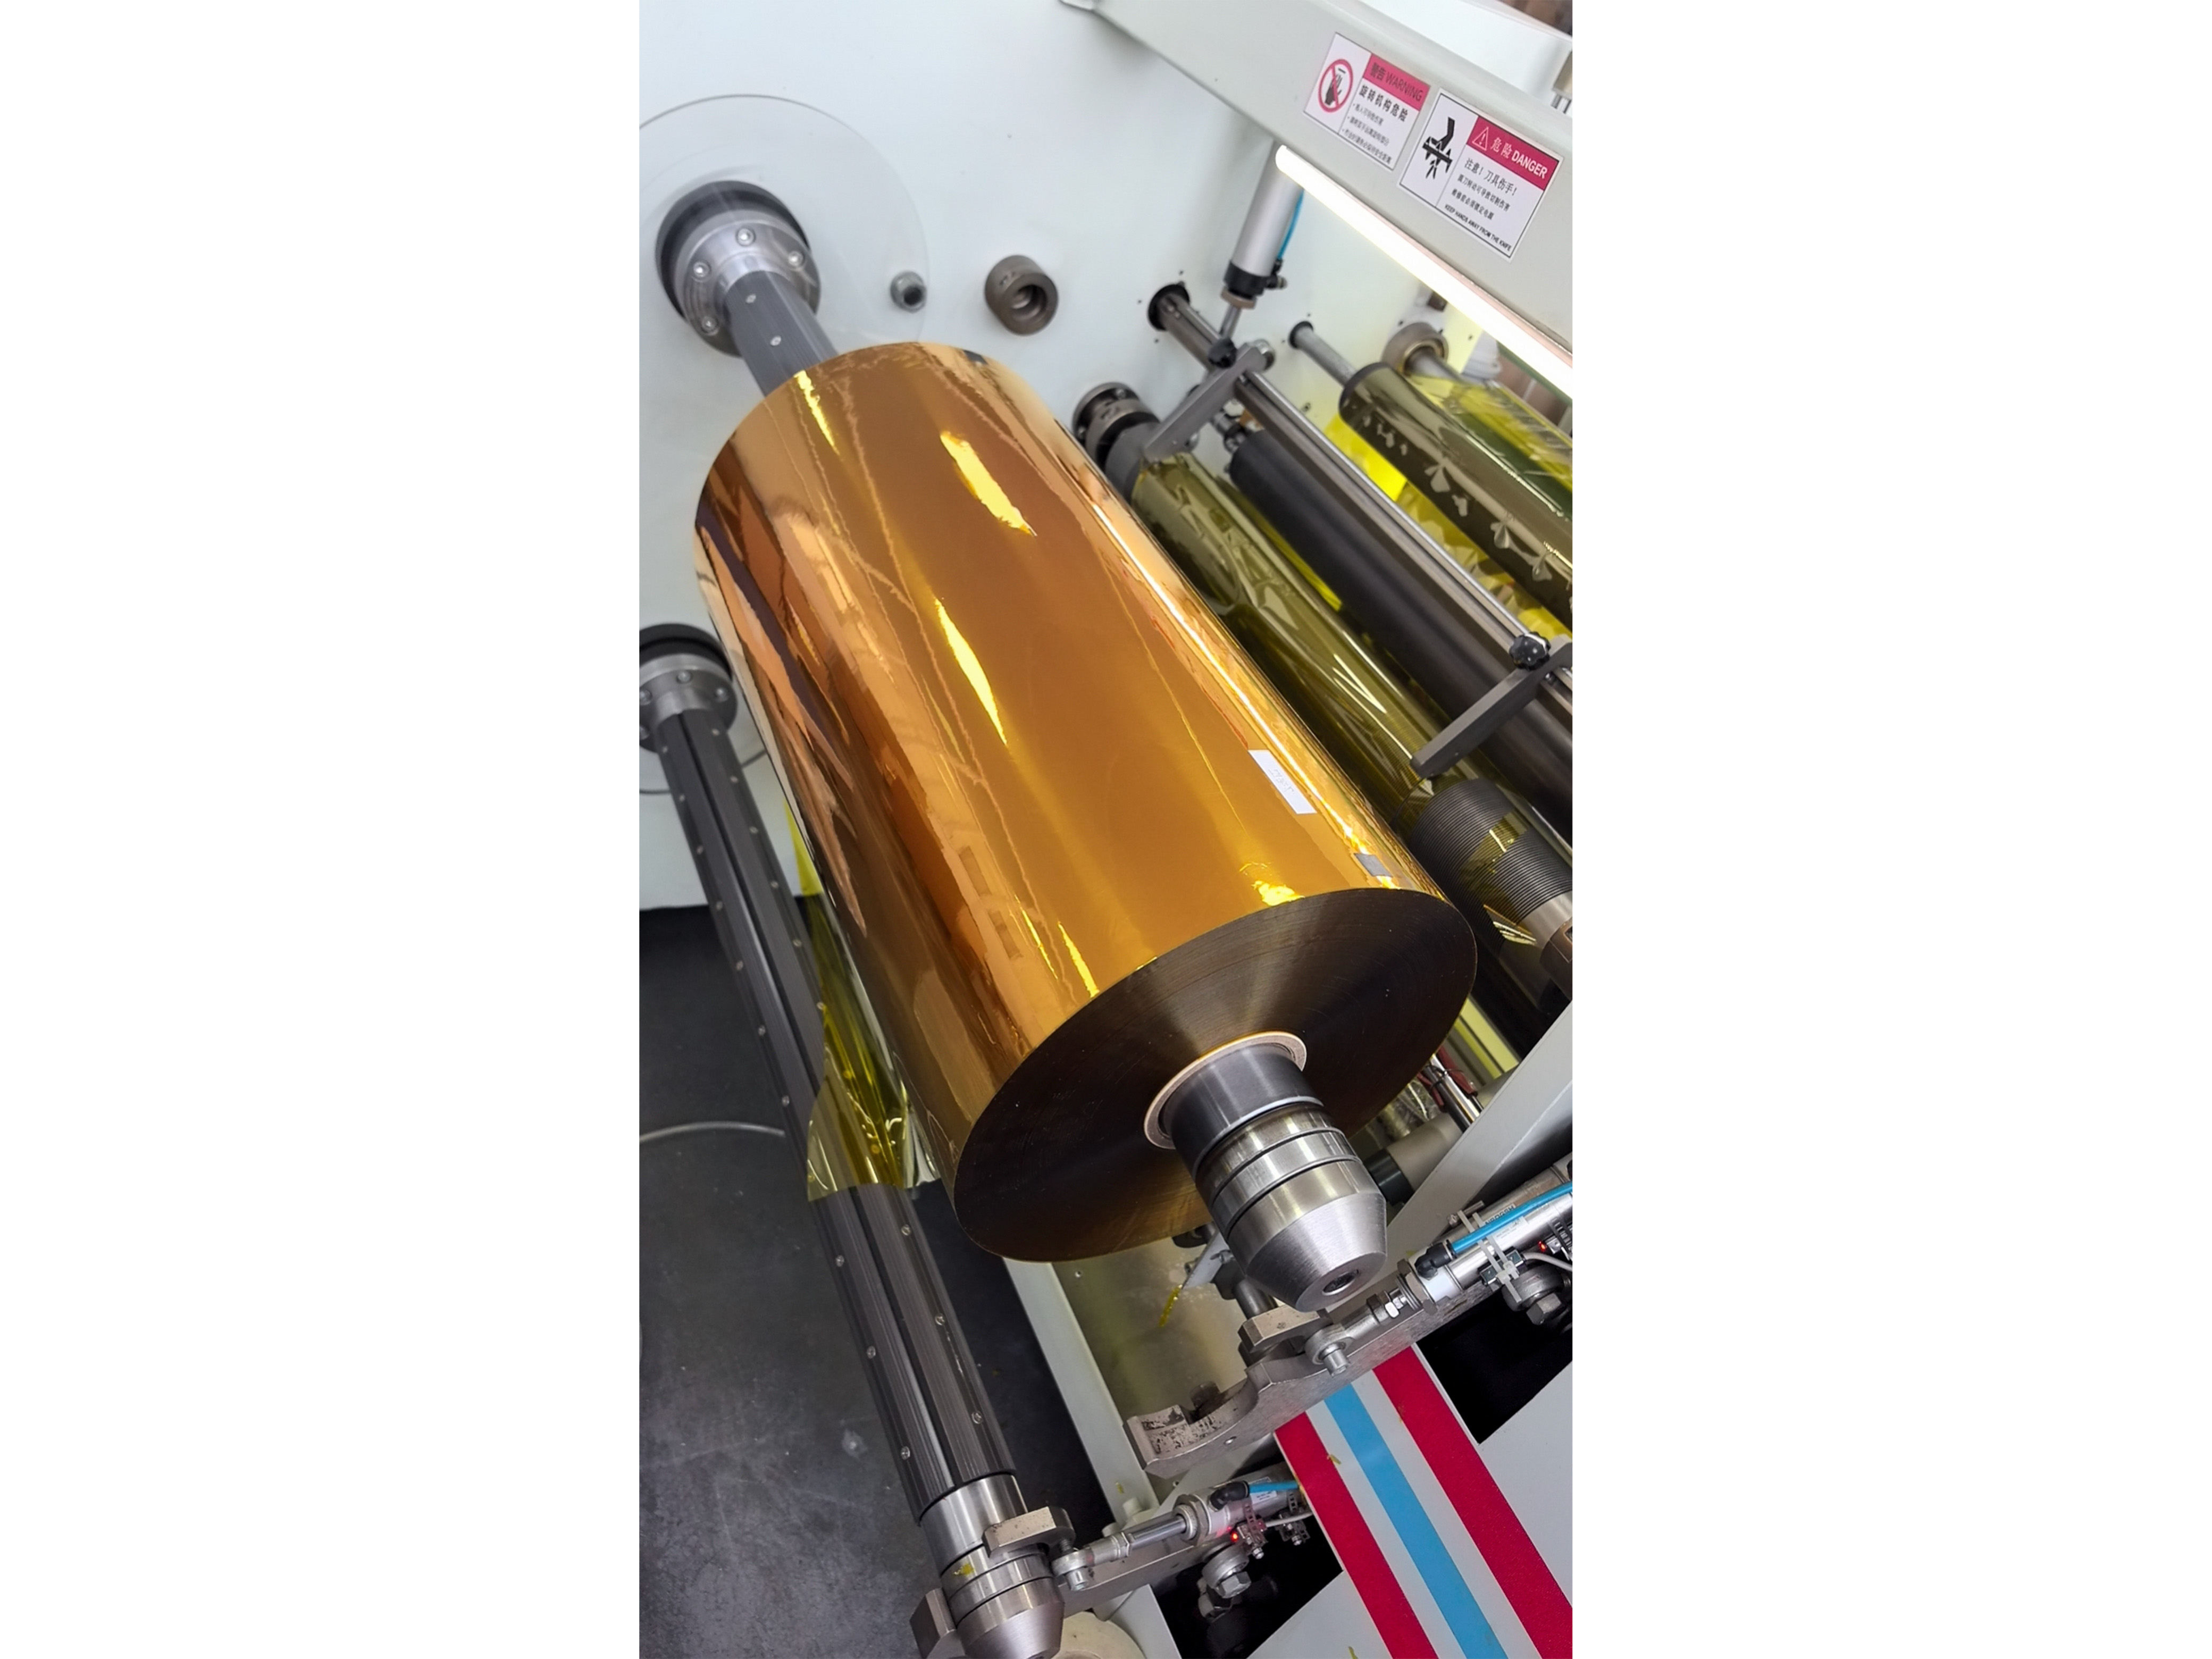
Select sharp and smooth hard alloy slitting knives, and adjust the clearance between the knife shafts according to the thickness of the film. Blade passivation can cause cutting edge drawing, burrs, and film delamination. Regular inspection and grinding of cutting tools are required according to the production plan; Debugging the knife pressure. If the knife pressure is too high, it will cause pressure marks on the squeezed film. If the pressure is insufficient, it is easy to have continuous cutting and uneven cutting.
4. Control operating speed and temperature environment
Maintain stable cutting speed to avoid sudden acceleration or shutdown. Speed fluctuations can easily cause film shaking, resulting in oblique cuts and varying lengths. The temperature and humidity in the workshop environment remain stable. If the ambient temperature is too high, it will affect the release of film stress. Abnormal humidity will change the friction characteristics of the film surface, causing winding slip and uneven end faces.
5. Roll up process control
When winding, keep the end face of the film roll flat, select a suitable winding core tube, and keep the surface of the core tube clean. The winding pressure is uniform, and excessive pressure can easily cause extrusion stress on the inner film, resulting in loose rolls and curled edges during later storage; If the pressure is too low, there will be roll slip and end face misalignment. Flattening rollers can be installed on the winding side as needed to reduce wrinkles.
6. Electrostatic protection
Friction during the cutting process of polyimide film can easily accumulate static electricity, which can adsorb dust and cause film adhesion. In severe cases, it can cause surface damage to the film. The equipment can be equipped with static elimination devices, and at the same time, the equipment should be grounded to control workshop dust and reduce the adverse effects of static electricity.
7. Semi finished product testing and labeling
During the slitting process, regular spot checks are conducted on the appearance and width tolerance of the cut, and the stretching direction of the film roll is recorded. Direction markings are made on the outer side of the finished roll to facilitate downstream customers' subsequent processing and use. Pay attention to whether there are scratches, pinholes, wrinkles and other defects on the surface of the film, and promptly investigate any abnormalities caused by equipment and raw materials.
8. Storage and Protection
The finished film roll after slitting should be wrapped and protected to reduce direct exposure to the environment. The placement method of the film roll should avoid compression, prevent stress accumulation, and affect subsequent secondary processing such as customer compounding and die-cutting.
 WeChat number:
 Home
 Product
 Wechat
 Telephone